
High Performance Reverse Osmosis Plant Manufacturers in Pune
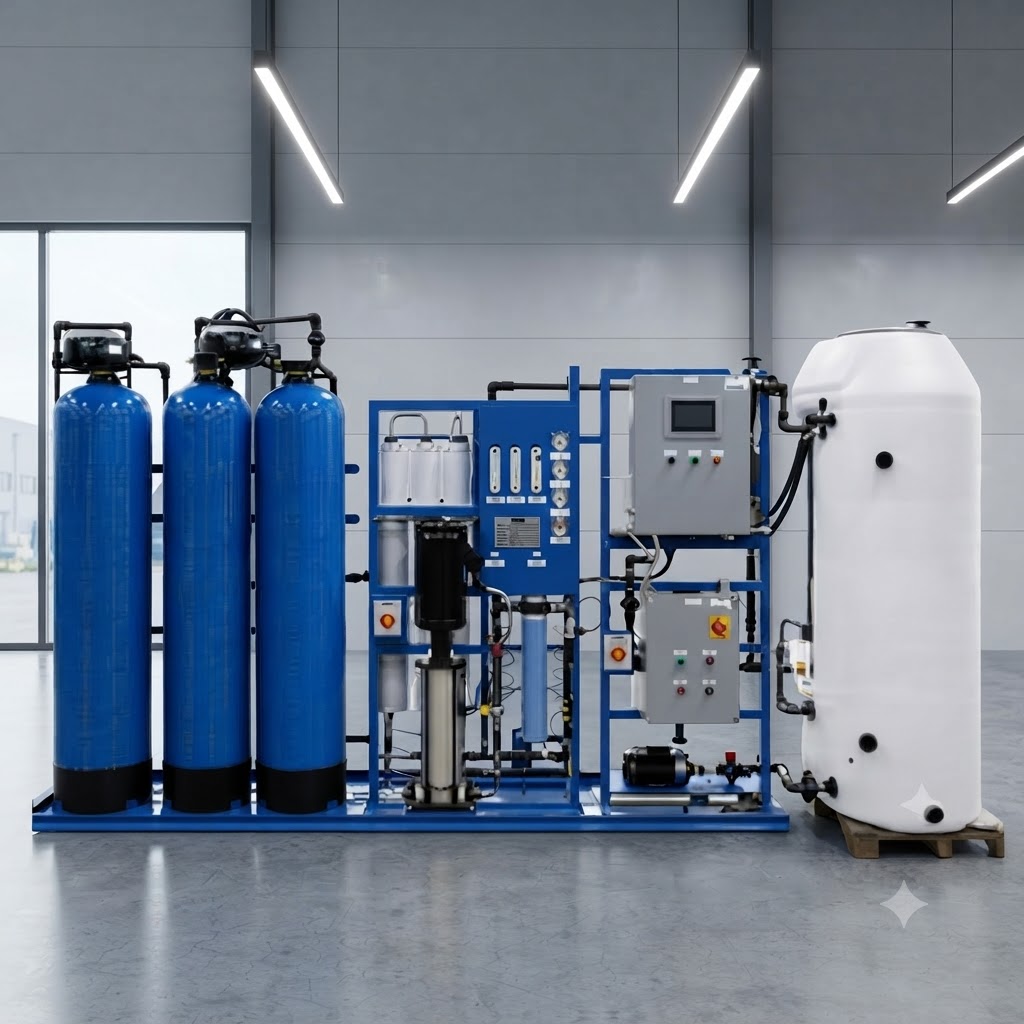
Bluematrix Water is leading Reverse Osmosis Plant Manufacturers, Suppliers and Service Providers in Pune. We are committed to delivering dependable water treatment solutions with quality, practical design, competitive pricing, and application-focused capabilities.
Our approach combines technical understanding, precision manufacturing, and customer-oriented service to meet diverse water purification requirements. We offer solutions designed for residential, commercial, and industrial needs, with attention to performance, durability, and ease of operation.
Customers choose us for our quality-driven approach, responsive support, customization capability, and commitment to delivering reliable solutions that provide long-term value.
Reverse Osmosis Plant Service Providers in Pune
As trusted provider of Reverse Osmosis Plant Services in Pune, we can support customers with application-oriented RO solutions from system selection through installation and service.
- RO Plant Design & Supply: We help select suitable treatment stages, capacity, membrane configuration, and equipment according to feed-water quality and daily water demand with Turnkey Reverse Osmosis Plants.
- Installation & Commissioning: Our service approach supports proper equipment installation, system testing, commissioning, and operational guidance for dependable performance.
- RO Plant Maintenance: Preventive inspection, filter servicing, membrane care, pressure checks, and performance monitoring help maintain efficient operation.
- Customized Water Treatment Solutions: We can develop application-specific systems for different capacities, water conditions, and industrial process requirements.
How Does a Reverse Osmosis Plant Work?
A reverse osmosis (RO) plant purifies water through a systematic multi-stage process. In a typical Reverse Osmosis Water Treatment Plant, pre-treatment protects the membranes, while high-pressure membrane filtration removes dissolved impurities and produces purified water.
- Raw Water Collection: The process begins when incoming water is collected in a raw water tank. This provides a consistent feed supply for the complete treatment system.
- Pre-Treatment: Water passes through a pressure sand filter and activated carbon filter to reduce suspended particles, chlorine, colour, odour, and other substances that could affect membrane performance.
- Micron Filtration: The water then passes through a micron or cartridge filter that captures fine particles and provides additional protection to the RO membranes and downstream equipment.
- High-Pressure Feeding: A high-pressure pump increases the water pressure to the level required for membrane filtration. This pressure enables water to pass through the semi-permeable membrane effectively.
- RO Membrane Separation: At the core of the Industrial Reverse Osmosis Plant, water is forced through semi-permeable RO membranes. The membranes allow purified water to pass while rejecting many dissolved solids, salts, heavy metals, and contaminants.
- Purified Water Collection: The treated water, known as permeate, is collected after membrane separation and transferred to a storage tank. It can then be supplied for drinking, process, or other suitable applications.
- Reject Water Management: The concentrated water containing rejected impurities is separated as reject water. Depending on the application, it can be safely discharged, treated further, or managed through an appropriate recovery and reuse system.
Types of Reverse Osmosis Plant
As Reverse Osmosis Plant Manufacturers in Pune, we provide thoughtfully designed RO solutions across residential, commercial, industrial, and specialized water treatment requirements.
- Residential RO System: It is a compact Ro Plant designed for homes, providing purified drinking water through a space-saving multi-stage filtration process. It is suitable for kitchens and household applications where reliable water purification is required for regular daily consumption.
- Commercial RO Plant: It is a medium-capacity Commercial RO Plant designed for offices, schools, hospitals, hotels, and apartments with higher daily water requirements. It provides consistent treated water and can be configured according to capacity, feed-water quality, and specific commercial needs.
- Industrial RO Plant: It is a heavy-duty Industrial RO Plant developed for factories, manufacturing facilities, and large-scale processing operations requiring dependable water treatment. It can be customized as an Industrial RO Water Treatment Plant according to production demand, feed-water conditions, and required water quality.
- Brackish Water RO Plant: It is a specialized Reverse Osmosis Water Treatment Plant designed to treat brackish or borewell water containing elevated levels of dissolved salts and TDS. It uses suitable RO membranes and pre-treatment stages to reduce dissolved impurities and produce water for industrial or commercial applications.
- Seawater RO (SWRO) Plant: It is a high-pressure RO Water Purification Plant designed to desalinate seawater containing high concentrations of dissolved salts. It uses specialized membranes and robust pumping equipment to produce freshwater from seawater for suitable applications.
- Portable RO Plant: It is a compact high-capacity water purification system available in movable or skid-mounted configurations for locations requiring flexible water treatment. It is suitable for temporary sites, remote locations, field operations, and emergency applications where a portable RO Water Plant is required.
Components of a Reverse Osmosis Plant
As Reverse Osmosis Plant Suppliers in Pune, we offer carefully selected RO components that support efficient filtration, reliable operation, easy monitoring, and consistent water treatment performance.
| Component | Function |
|---|---|
| Raw Water Tank | Stores incoming water and provides a controlled supply to the treatment system. |
| Feed Pump | Transfers raw water from the tank toward the pre-treatment stages at the required flow. |
| Pressure Sand Filter | Removes suspended solids and larger particulate matter from incoming water. |
| Activated Carbon Filter | Helps reduce chlorine, organic matter, colour, and unpleasant odour before RO treatment. |
| Micron/Cartridge Filter | Provides fine filtration and protects the RO membranes from remaining particles. |
| High-Pressure Pump | Generates the operating pressure needed for membrane separation. |
| RO Membranes | Perform the core separation process by allowing water to pass while rejecting many dissolved impurities. |
| Membrane Housings | Secure and protect the RO membranes while directing feed, permeate, and reject flows. |
| Flow Meters | Monitor water flow through important sections of the treatment system. |
| Pressure Gauges | Display operating pressure and help identify abnormal pressure conditions. |
| Control Panel | Provides centralized control and monitoring of pumps and system functions. |
| Dosing System | Adds required treatment chemicals in controlled quantities where the application demands it. |
| CIP System | Supports cleaning of membranes and associated components to help maintain performance. |
| Storage Tank | Stores purified water for controlled distribution and subsequent use. |
Key Features of Reverse Osmosis Plant
As Reverse Osmosis Plant Manufacturers in Pune, we focus on combining efficient filtration, practical engineering, flexible capacities, and dependable components to meet diverse water purification requirements.
- Efficient Membrane Filtration: Our reverse osmosis (RO) plant uses advanced membrane technology to reduce dissolved solids, salts, heavy metals, and other unwanted contaminants from feed water.
- Customized Treatment Capacity: We can configure each RO Water Plant according to water demand, feed-water quality, required recovery, and the specific needs of commercial or industrial applications.
- Multi-Stage Pre-Treatment: The system incorporates suitable filtration stages to protect RO membranes from suspended particles, chlorine, hardness-related issues, and other substances that can affect performance.
- Reliable Monitoring and Control: Flow meters, pressure gauges, control panels, and other instruments help operators monitor important operating conditions for smooth and efficient system performance.
- Durable Industrial Construction: Our Industrial RO Plant solutions can be designed with suitable materials and components to support dependable operation in demanding water treatment environments.
Benefits of Reverse Osmosis Plant
As Reverse Osmosis Plant Suppliers in Pune, we deliver water treatment solutions designed to improve purification efficiency, support consistent water quality, and provide practical value for different applications.
- Improved Water Quality: Our RO systems remove impurities effectively, helping produce cleaner and more consistent treated water for a wide range of applications.
- Reduced Dissolved Contaminants: The RO membrane process helps reduce TDS, dissolved salts, heavy metals, and other contaminants that may affect water quality.
- Consistent Purification: A properly designed Reverse Osmosis Water Treatment Plant provides a controlled treatment process that supports consistent purified-water production.
- Suitable for Multiple Industries: RO technology can be adapted for commercial facilities, manufacturing units, pharmaceutical processes, food production, textile operations, and other industries.
- Better Process Efficiency: Proper pre-treatment, membrane selection, and regular maintenance can support efficient operation while helping extend the useful service life of key components.
Applications of Reverse Osmosis Plant
As Reverse Osmosis Plant Manufacturers in Pune, we develop versatile RO solutions that can support water purification requirements across commercial facilities, industries, institutions, and specialized processing sectors.
- Commercial Water Treatment: Our Commercial RO Plant is suitable for offices, schools, hotels, hospitals, apartments, and commercial buildings requiring a dependable supply of purified water.
- Manufacturing Industries: An Industrial RO Water Treatment Plant can provide treated water for manufacturing processes, utilities, equipment operation, and other industrial requirements.
- Pharmaceutical Water Treatment: RO systems can serve as an important purification stage for pharmaceutical facilities where controlled water quality is required for production and utility applications.
- Textile Water Treatment: A RO Water Purification Plant can help provide suitable-quality water for textile processing, dyeing, washing, and related industrial operations.
- Food Industry Water Treatment: RO technology can support food and beverage facilities by providing purified process water for suitable production and cleaning applications.
- Chemical Industry Water Treatment: Industrial RO systems can reduce dissolved contaminants from feed water used in selected chemical manufacturing and process applications.
- Hospital Water Treatment: RO treatment can be used in suitable hospital water-treatment applications where improved water quality is required for specific processes and utilities.
- Municipal and Institutional Water Treatment: A Reverse Osmosis Water Treatment Plant can be integrated into suitable institutional or municipal systems to improve water quality and reduce dissolved contaminants.
Why Choose Us?
- Application-Focused RO Solutions: We understand that every water source and treatment requirement is different, so we focus on delivering appropriately configured RO solutions based on capacity, water quality, and intended application.
- Quality with Practical Value: We combine quality-focused engineering, suitable components, and competitive pricing to provide dependable water treatment solutions that deliver practical value over the long term.
- Responsive Technical Support: We support customers with clear technical guidance, system selection, installation assistance, and maintenance-oriented service to help keep the Industrial RO Water Treatment Plant operating efficiently.
Choose Bluematrix Water is prominent Reverse Osmosis Plant Manufacturers, Suppliers and Service Providers in Pune. We provide water treatment solutions designed around real operating requirements, water quality, capacity, and application needs. Our focus is on quality, practical engineering, dependable performance, and customer support. Whether the requirement is a commercial purification system or an industrial installation, we work toward delivering an efficient solution that supports reliable water treatment and long-term operating value. Reach out to us for further details.
FAQ’s
A Reverse Osmosis Plant uses pressure to push water through semi-permeable membranes that separate many dissolved salts, solids, and contaminants. The purified permeate is collected for use, while concentrated reject water is discharged or managed separately.
RO systems are used for drinking water, process water, industrial utilities, and commercial purification requirements. Typical sectors include manufacturing, hotels, pharmaceuticals, food processing, textiles, and chemical industries.
Capacity should be selected according to daily water demand, peak consumption, operating hours, feed-water quality, and required treated-water quality. A proper water analysis and application assessment help determine the suitable plant size.
The cost depends on capacity, membrane configuration, construction material, automation, pre-treatment, pumps, and site requirements. For example, the 1000 liters Ro Plant Price can vary significantly depending on the final system specification.
Pre-filters generally require more frequent attention, while membranes need periodic cleaning and performance checks. Actual membrane replacement intervals depend on feed-water quality, pre-treatment, operating conditions, cleaning practices, and usage.

