
Demineralization (DM) Plant Manufacturers in Pune
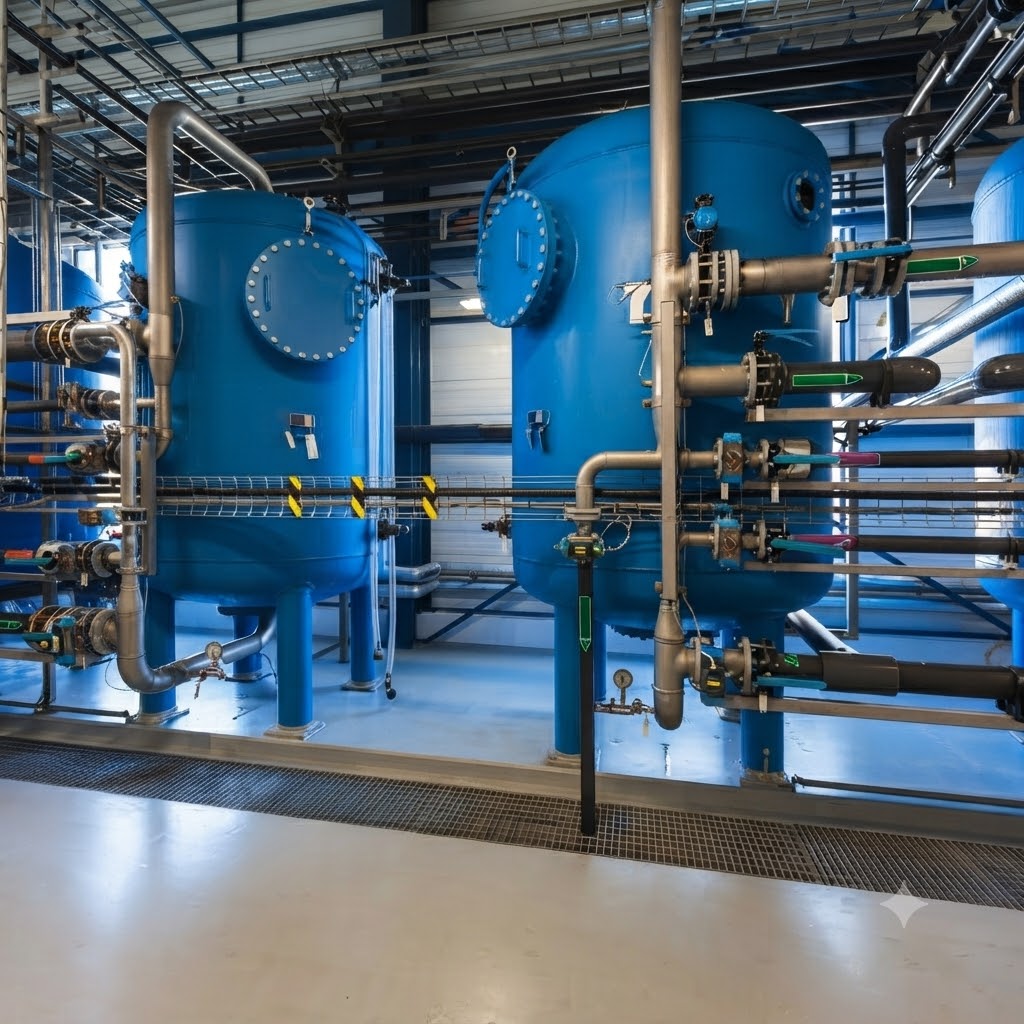
Bluematrix Water is leading Demineralization (DM) Plant Manufacturers, Suppliers and Service Providers in Pune. We provide reliable and customized Industrial DM Plant solutions designed around specific industrial requirements.
We focus on quality engineering, dependable components, competitive pricing, and practical system design. Our expertise covers design, manufacturing, installation, commissioning, operation, and maintenance support. We deliver solutions for different water qualities, capacities, and applications while maintaining a strong focus on performance and long-term value.
With our experienced technical team and customized approach, we help industries achieve consistent treated-water quality through efficient and professionally engineered systems. Our Demineralisation system solutions are developed to meet varying industrial water-treatment requirements with dependable performance and practical engineering.
Demineralization (DM) Plant Service Providers in Pune
We provide customized DM plant service in Pune for industries requiring low-mineral, high-quality treated water. We design and deliver systems based on feed-water quality, capacity, application, and site requirements.
- Customized Design: DM plants are engineered to match water chemistry, flow rate, purity requirements, and available space.
- Quality Manufacturing: We manufacture systems with suitable resins, vessels, valves, piping, instruments, and controls for reliable operation.
- Installation & Commissioning: Our team handles installation, testing, commissioning, and operational support for smooth plant startup.
- Maintenance Support: We provide servicing, troubleshooting, and technical assistance to maintain efficient and consistent plant performance.
How Does a Demineralization (DM) Plant Work?
A DM Water Plant uses ion exchange to remove dissolved salts, minerals, and ionic impurities from water. The treatment typically involves cation exchange, anion exchange, and optional polishing to produce low-mineral water for industrial applications. The system commonly uses ion exchange resin-based demineralization columns to achieve effective removal of dissolved ionic impurities.
- Feed Water Entry: Raw or pretreated water enters the DM system at a controlled flow rate for effective treatment.
- Cation Exchange: Cation resin removes positively charged ions such as calcium, magnesium, sodium, and iron by exchanging them with hydrogen ions.
- Degassing: Where required, a degasser reduces dissolved carbon dioxide before the anion treatment stage, improving overall process efficiency.
- Anion Exchange: Anion resin removes negatively charged ions such as chloride, sulphate, and bicarbonate by exchanging them with hydroxide ions.
- Polishing: A mixed-bed unit can be added for final polishing to achieve higher-purity, low-conductivity demineralized water.
- Treated Water Collection: The treated water is collected and supplied for applications such as boiler feed water, pharmaceutical processing, and industrial manufacturing.
- Resin Regeneration: When the resins become exhausted, they are regenerated with suitable chemicals and rinsed to restore their ion-exchange capacity.
Overall, the Conventional DM Plant Process provides an efficient water treatment system that removes dissolved salts, ions, and impurities, helping industries maintain consistent water quality and protect sensitive equipment.
Types of Demineralization (DM) Plant
As Demineralization (DM) Plant Manufacturers in Pune, we offer multiple DM plant configurations designed to meet different feed-water conditions, purity requirements, capacities, and industrial applications.
These DM Plant (De Mineralization Plant) Water Treatment Plants can be configured according to required capacity, feed-water characteristics, and treated-water quality.
- Two-Bed Demineralization Plant: A two-bed DM plant uses separate cation and anion exchange vessels, with an optional degasser between them to improve treatment efficiency. It is widely used for industrial applications requiring reliable demineralized water with controlled conductivity.
- Mixed-Bed Demineralization Plant: A mixed-bed DM plant combines cation and anion exchange resins in a single vessel for final water polishing. It produces high-purity, low-conductivity water for applications where stricter water quality is required.
- Ion Exchange Demineralization Plant: An ion exchange DM plant uses specialized resins to exchange dissolved cations and anions, significantly reducing mineral content. Its configuration can be selected according to feed-water quality, flow capacity, and required treated-water specifications.
- RO-Based Demineralization Plant: This system combines Reverse Osmosis with mixed-bed ion exchange or EDI to reduce dissolved solids before final demineralization. It offers an efficient solution for high-purity water production with reduced chemical regeneration requirements.
- RO-EDI Demineralization Plant: RO-EDI systems use Reverse Osmosis as pre-treatment followed by electro deionization for continuous ionic removal and polishing. This configuration is suitable for industries requiring consistent ultra-pure water with minimal chemical handling.
We provide High-quality Demineralization (DM) Plants for industrial water and wastewater treatment, with configurations tailored to specific process and utility requirements, including 1000 LPH DM, 5000 LPH DM, 10000 LPH, and 50000 LPH DM water plant capacities.
Components of a Demineralization (DM) Plant
As Demineralization (DM) Plant Suppliers in Pune, we provide carefully selected and quality-engineered components to ensure efficient ion removal, reliable operation, and consistent demineralized water quality.
| Component | Function |
|---|---|
| Cation Exchange Vessel | Holds cation resin for removing positively charged dissolved ions. |
| Anion Exchange Vessel | Contains anion resin for removing negatively charged dissolved ions. |
| Mixed Bed Vessel | Provides final polishing when higher water purity is required. |
| Ion Exchange Resins | Perform the primary ion-exchange process for mineral removal. |
| Valves & Piping | Control water flow, regeneration, rinsing, and service cycles. |
| Chemical Dosing / Regeneration System | Supplies regeneration chemicals required to restore resin capacity. |
| Degasser | Helps reduce dissolved carbon dioxide where included in the process design. |
| Flow & Pressure Instruments | Help operators monitor important operating parameters. |
| Control Panel | Supports controlled and convenient plant operation. |
| Treated Water Storage | Stores demineralized water for continuous or intermittent industrial use. |
Key Features of Demineralization (DM) Plant
As Demineralization (DM) Plant Manufacturers in Pune, we engineer our DM plants with practical features that support efficient performance, easy operation, flexible capacity, and long-term industrial reliability.
- Customized Plant Design: We design each DM Plant according to feed-water quality, required capacity, treated-water specifications, and industrial operating conditions.
- Efficient Ion Removal: Advanced ion exchange technology effectively removes dissolved salts, minerals, and unwanted ions to produce consistent demineralized water.
- Robust & Low-Maintenance Construction: Our systems are engineered with durable components to support reliable performance, easy servicing, and reduced maintenance requirements.
- Flexible Capacity Options: We provide suitable configurations for applications ranging from smaller process requirements to large-scale industrial water treatment operations.
- Integrated Treatment Solutions: Our Demineralization (DM) Water Treatment Plants can be integrated with RO, filtration, softening, storage, and other treatment equipment for complete water management.
Benefits of Demineralization (DM) Plant
As Demineralization (DM) Plant Suppliers in Pune, we deliver solutions that help industries achieve consistent water quality, protect equipment, improve process efficiency, and manage long-term treatment requirements effectively.
- High-Quality Treated Water: The system efficiently reduces dissolved minerals and ionic impurities, providing water suitable for demanding industrial processes.
- Protects Industrial Equipment: Low-mineral water helps reduce scaling, deposits, and corrosion-related problems in boilers, pipelines, heat exchangers, and process equipment.
- Improves Process Reliability: Consistent water quality supports stable production and helps maintain dependable performance across industrial operations.
- Cost-Effective Water Treatment: Properly designed industrial DM Plant systems can reduce water-related maintenance issues and support efficient long-term plant operation.
- Suitable for Multiple Industries: DM technology provides a versatile solution for industries requiring controlled-quality water for production, utilities, and process applications.
Applications of Demineralization (DM) Plant
As Demineralization (DM) Plant Manufacturers in Pune, we design DM solutions for diverse industries where low-mineral, low-conductivity, and consistently treated water is essential for production and utility operations.
- Boiler Feed Water: A DM plant for boiler feed water supplies low-mineral water that helps minimize scaling and supports efficient boiler operation.
- Pharmaceutical Industry: DM water is used where controlled mineral content and consistent water quality are important for manufacturing and process applications.
- Chemical Industry: Demineralisation systems support chemical processes that require water with reduced dissolved salts and ionic impurities.
- Textile Industry: DM water helps maintain consistent process conditions in dyeing, washing, finishing, and other textile manufacturing operations.
- Food & Beverage Industry: Treated water can support production and utility processes where controlled mineral content is required for consistent operation.
- Power & Utility Plants: DM systems provide suitable water for boilers and other applications that require low-conductivity process or utility water.
- Electronics & Manufacturing: High-purity water produced through ion exchange demineralization plants can be used for specialized manufacturing and cleaning processes.
- General Industrial Applications: A DM water treatment plant can be customized for diverse industries requiring reliable removal of dissolved salts, minerals, and ions from water.
We provide end-to-end solutions for demineralized (DM) water systems, from initial design and manufacturing through installation, commissioning, and after-sales support. We can also support a DM plant turnkey project, covering the major stages from engineering and manufacturing to installation and commissioning.
Why Choose Us?
- Expertise in Customized Water Treatment: We develop customized water treatment and DM plants based on actual feed-water conditions, capacity requirements, and specific industrial applications.
- Quality with Competitive Value: We combine dependable components, practical engineering, and competitive pricing to deliver efficient DM solutions focused on long-term operational value.
- Complete Project Support: We provide end-to-end assistance covering design, manufacturing, installation, commissioning, technical guidance, and after-sales support for dependable plant operation.
Choose Bluematrix Water is prominent Demineralization (DM) Plant Manufacturers, Suppliers and Service Providers in Pune. We provide reliable DM Water Plant solutions designed to deliver consistent demineralized water for diverse industrial requirements. With customized engineering, quality-focused construction, competitive pricing, and complete technical support, we help customers achieve efficient, dependable, and long-lasting water treatment performance across their operations. Get in touch with us for additional details.
FAQ’s
A DM plant removes dissolved ions and mineral salts from water using cation and anion exchange resins. The process produces low-mineral water suitable for industrial and utility applications.
DM plants are commonly used for boiler feed water, manufacturing, chemical processing, pharmaceuticals, and sensitive industrial processes. They are selected wherever reduced dissolved mineral content is important for water quality.
Capacity should be selected according to water consumption, peak flow, operating hours, feed-water quality, and required treated-water quantity. Our technical team can help determine a suitable configuration from smaller systems to large industrial capacities.
The cost depends on capacity, feed-water chemistry, resin quantity, vessel material, automation, regeneration arrangement, and required water quality. For an accurate quotation, the plant should be sized according to the project's technical requirements rather than using a fixed price.
Routine inspection, regeneration-system checks, valve servicing, and water-quality monitoring help maintain reliable performance. Resin replacement depends on feed-water quality, operating conditions, regeneration efficiency, and resin life, so it should be based on actual performance.

